🔩 Tool Wear Reduction — WinFusion 2025
Tool Wear Reduction Tips —
5-Axis Blade Machining Mein Tool Life Kaise Improve Karein? 🔩
Adaptive Roughing | Rest Machining | Tool Axis | Overhang | Chip Evacuation | Simulation
Frequent Tool Change Ka Real Cost:
Cutter Cost ⬆️
₹ Per edge
Scrap Risk ⚠️
Part reject!
5-axis blade machining mein tool wear sirf RPM ya feed se fix nahi hota — engagement control, tool axis angle, overhang, chip evacuation aur rest machining sab important hain. WinFusion workflow se sab systematically address karo!
Har kuch parts ke baad cutter change karna pad raha hai? Surface finish inconsistent aa rahi hai, ya finishing ke end tak tool dull ho jaata hai? Tool wear ka solution sirf RPM ya feed kam karna nahi hota — blade machining mein cutter ka contact, angle, overhang aur chips ka management sab dekhna padta hai! WinFusion workflow se ye sab systematically improve hota hai!
“CAM tool wear ko directly measure nahi karta — actual tool condition cutting ke baad inspect karke aur machine par process data dekhkar confirm karna hota hai. WinFusion CAM side ko optimize karta hai!” ✅
WinFusion workflow elements: Adaptive Roughing → Rest Machining → Tool Axis Control → Tool Library → Machine Simulation → Proven Post → Training + Trials. Har element ka alag role hai! ✅
🔍 Blade Machining Mein Tool Jaldi Wear Kyun Hota Hai?
Blade = simple flat surface nahi. Curved + changing angles = continuously changing tool engagement!
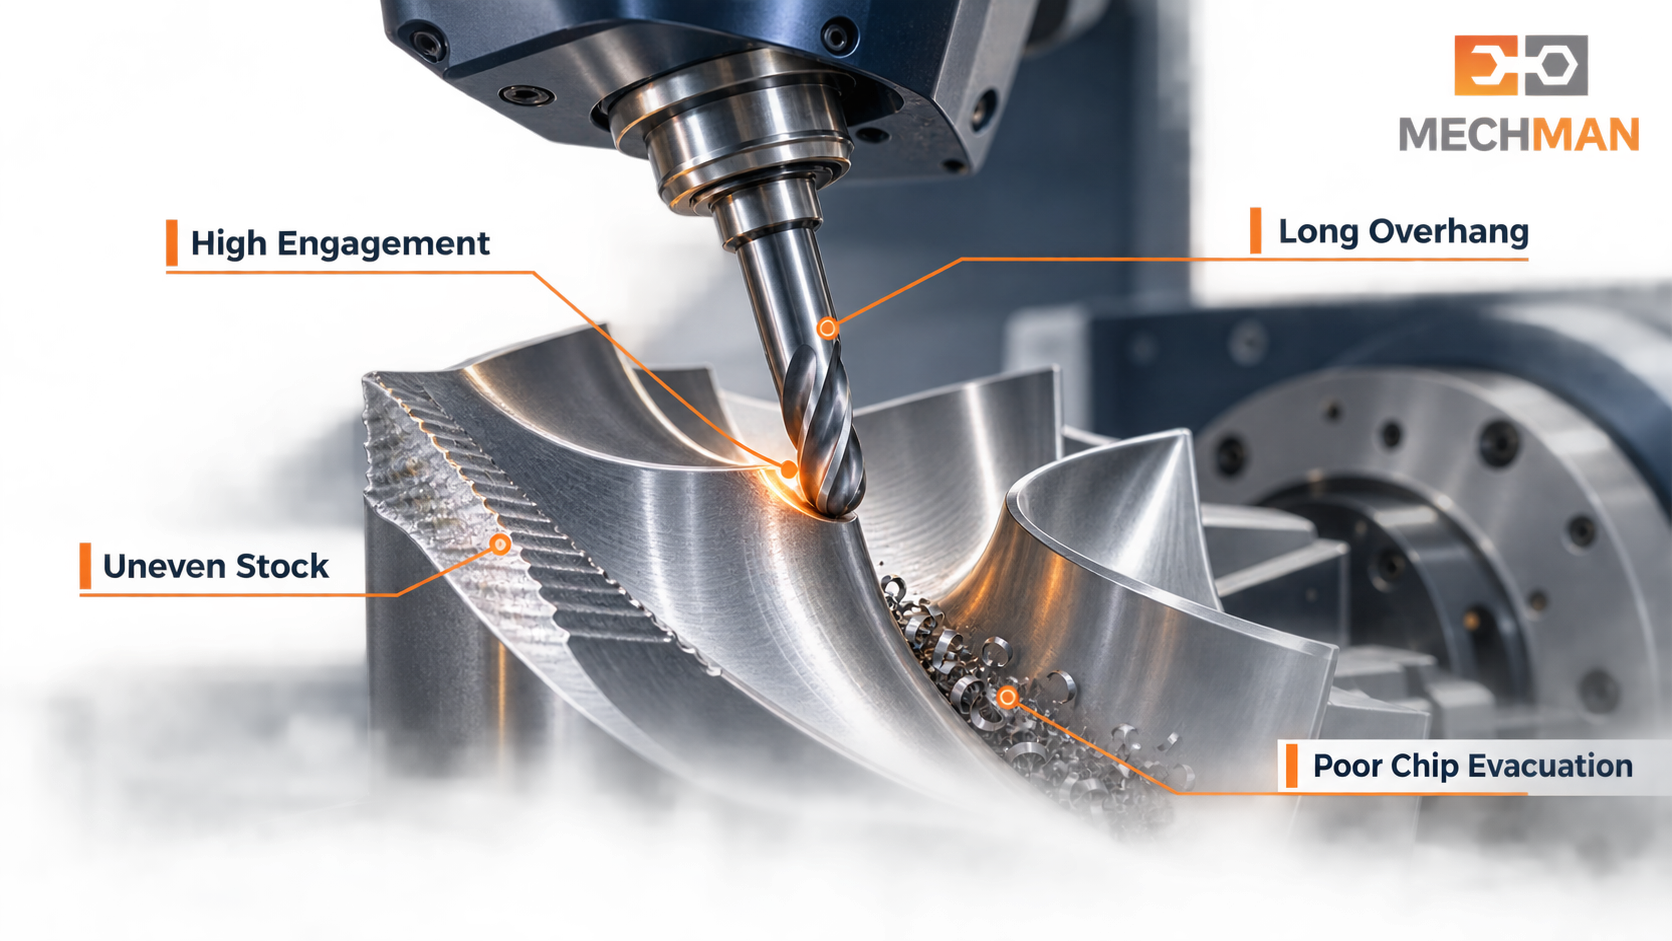
Blade mein tight curved area mein achanak engagement badh sakta hai — heat, chatter aur cutting-edge wear badhne ka risk! WinFusion workflow se is engagement ko predictable aur controlled rakhte hain!
⚠️Cutter engagement ka achanak badhna ⭐
⚠️Tool ka unnecessary long overhang
⚠️Ball-nose tip par zyada cutting ⭐
⚠️Poor chip evacuation + coolant
⚠️Roughing ke baad uneven stock ⭐
→9 tips se systematically fix karo! ✅
⚙️ 9 Practical Tips — Tool Life Improve Karo!
1
Roughing Mein Cutter Engagement Control Karo ⭐⭐
Conventional toolpath mein corner par achanak heavy engagement = cutting edge stress. Fusion 3D Adaptive Roughing relatively constant engagement maintain karta hai! Optimal Load tool manufacturer recommendation + material + machine capability ke hisaab se set karo.
❌ Conventional
Corner → sudden load → edge stress!
→
✅ Adaptive ⭐
Controlled engagement = less wear!
2
Roughing Ke Baad Uneven Stock Mat Chhodiye ⭐
Finishing cutter ko har jagah predictable material remove karna chahiye. Uneven stock = sudden load change = tool wear! Rest machining se locally remaining heavy areas remove karo.
Main Roughing
→
Rest Roughing ⭐
→
Semi-finish
→
Finish ✅
3
Tool Overhang Minimum Practical Length Par Rakhein ⭐
Lamba tool = deflection + vibration risk → uneven wear + poor finish. Lekin holder ko blade ya fixture se takrana bhi nahi chahiye. Tool length aur holder clearance saath plan karo!
Tip: Holder collision aane par first response sirf cutter lamba karna mat karo — suitable 5-axis tilt check karo. Better orientation = shorter + more rigid setup possible! ⭐
4
Tool-Axis Angle Ko Surface & Cutter Ke Hisab Se Set Karo ⭐⭐
5-AXIS KEY
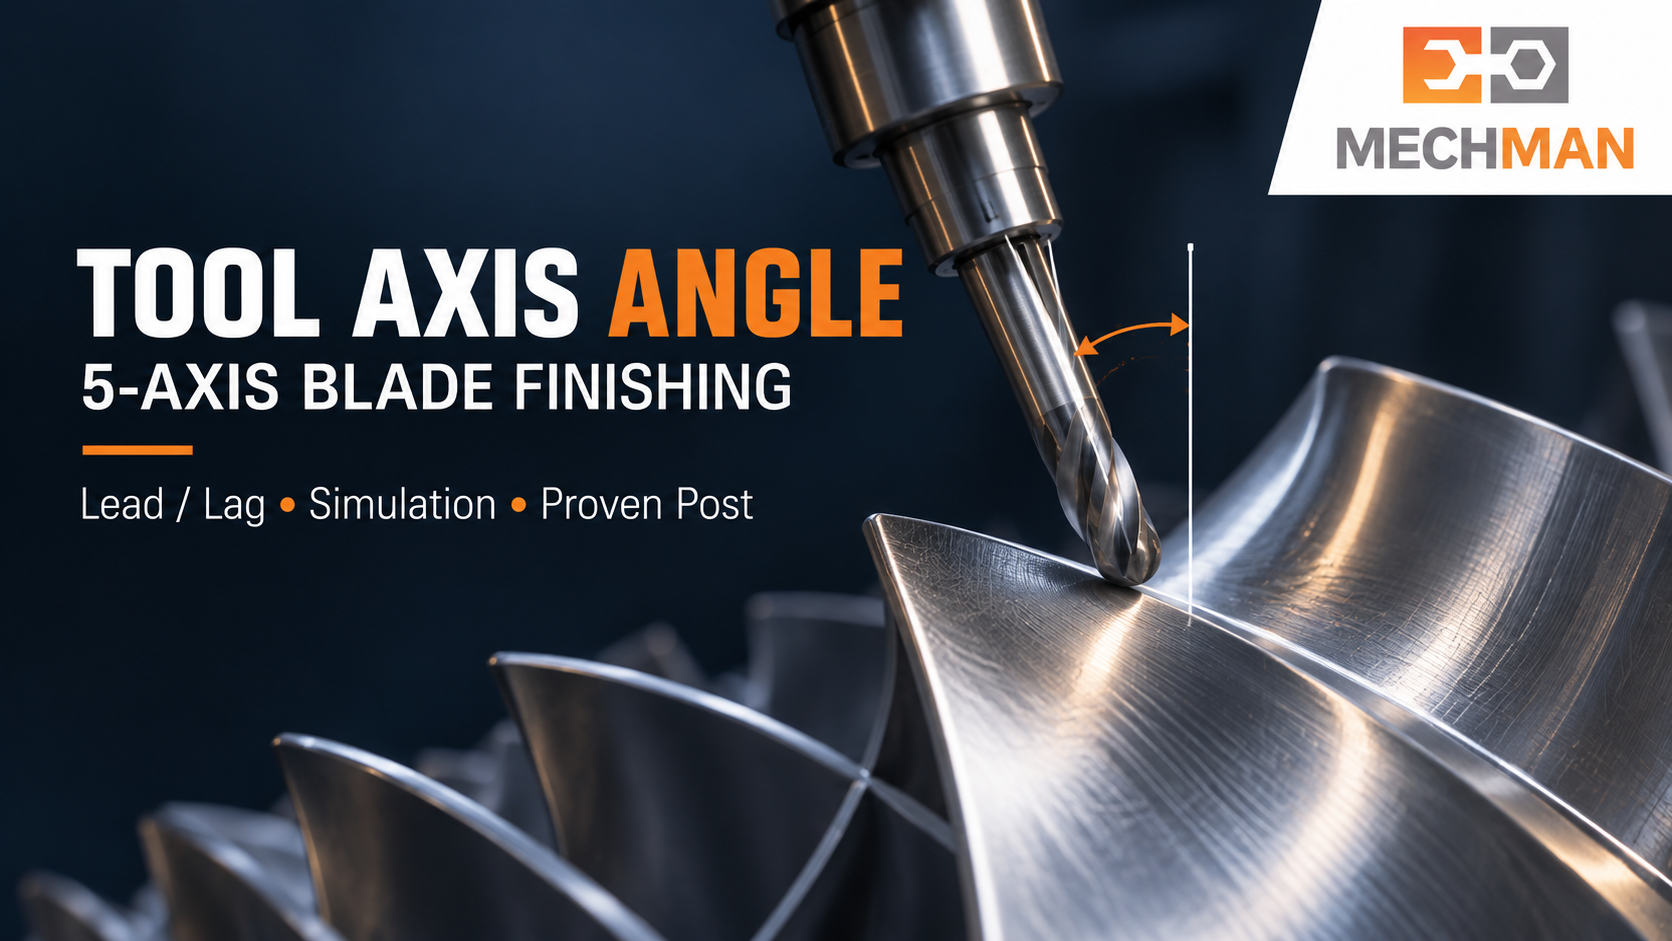
5-axis lead/lag angle: Ball-nose cutter ka effective cutting contact suitable part par aaye — tip rubbing avoid karo + adjacent blade clearance maintain karo + trial se verify karo!
Angle decide karte waqt check karo:
- Blade surface geometry ⭐
- Tool shape + diameter
- Adjacent blade clearance
- Machine rotary limits
Practical rule: ⭐
Sirf collision avoid karne ke liye set karke stop mat karo — actual cutting smooth hai ya chatter/rubbing? Trial cut se verify karo!
5
Tool Library Mein Real Tool Assembly Define Karo ⭐
Sirf nominal diameter dalna enough nahi — actual tool + shaft + holder + stick-out program se match karna chahiye. Wrong holder in simulation → misleading clearance results!
Cutter ⭐
Type, dia, radius, grade
Holder ⭐
Model + dimensions
Stick-out ✅
Actual protrusion
6
Speed & Feed Ko Wear Pattern Dekhkar Adjust Karo ⭐
Feed blindly reduce karna sahi diagnosis nahi hai — heat, rubbing, chatter, poor chip evacuation alag-alag reasons hain. First part ke baad inspect karo!
Edge wear uniform? ⭐
Spindle load spike?
Chips clean? ⭐
Sound consistent? ✅
7
Chip Evacuation & Coolant Delivery Check Karo ⭐
⚠️ Problem:
Chips wapas cutting zone mein → cutter chip ko dobara cut kare → tool damage. Blade ke narrow passages mein especially critical!
✅ Check:
Coolant nozzle direction, chip flow, cutting zone clearance — machine par observe karo! CAM simulation coolant actual flow nahi dikhata!
8
Simulation Se Collision & Unexpected Motion Pakdo ⭐
Simulation se: Tool/holder clearance check, excess stock identify, unsafe motion pakdo. Machine simulation mein linked model ho to machine movement + collision bhi verify hote hain!
✓Tool/holder clearance ⭐
✓Remaining stock verify
✓Tool axis smooth? ⭐
✓Rotary limits in range?
✓Post NC verified? ⭐
✓Machine trial! ✅
9
Tool Change Ko Guesswork Se Plan Mat Karo — Wear Log Rakhein ✅
“Tool 20 parts chalega” — fixed number reliable nahi hota. Material batch, setup, grade change honge to wear change hota hai! Simple wear log maintain karo:
Part #
Tool Condition
Finish
Action
First trial
Edge inspect ⭐
Reference note
Settings record
Next checks
Trend compare
Areas compare
Adjust if needed
Before limit
Verify wear ⭐
Acceptance check
Planned change ✅
📋 Program Release Se Pehle — 7-Point Quick Checklist!
Blade machining program release karne se pehle ye 7 checks zaroor karo:
☐
Tool manufacturer ke hisaab se cutter aur starting cutting data select kiya? ⭐
☐
Roughing engagement aur remaining stock inspect kiya? ⭐
☐
Rest machining ki need check ki? ⭐
☐
Actual holder aur stick-out tool library mein match kiya? ⭐
☐
Blade finishing ke tool-axis angles verify kiye? ⭐⭐
☐
Tool, holder, fixture aur machine simulation review ki? ⭐
☐
First part ke baad edge wear, finish aur chips record kiye? ✅
Tool Life Improve Karo — Systematically! 🔩
Controlled engagement + predictable stock + suitable tool-axis angle + rigid setup + first-part inspection = better blade tool life!
Blade Finish
✨ Consistent!
WinFusion: Adaptive Roughing + Rest Machining + Tool Axis + Tool Library + Simulation + Proven Post = Better Blade Tool Life! 🔩🚀
🔩
Tool Wear | Blade Machining | Tool Axis | Simulation | Post
Blade model, material, machine model, current tool details aur existing NC issue share karein!
Mechman Solutions — WinFusion
Autodesk Authorized Partner | Vadodara, Gujarat | Since 2015
www.mechmansolution.com
© 2025 Mechman Solutions | WinFusion — Tool Wear Reduction Tips: 5-Axis Blade Machining | Vadodara, Gujarat